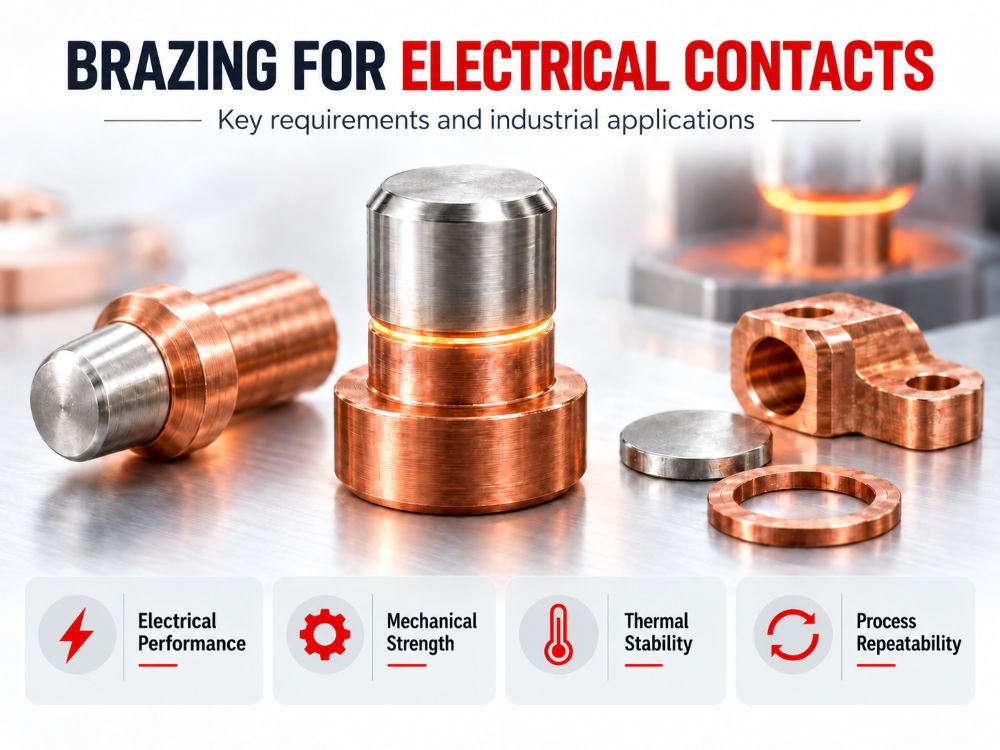
Materials, brazing alloys and process control for reliable electrical joints
In the electrical contact industry, the quality of the connection between different components is essential to ensure device reliability, service life and performance.
Relays, contactors, switches, terminals, protection devices and many other electrical components must operate under conditions involving:
- current flow;
- repeated thermal cycles;
- vibration;
- mechanical stresses;
- possible electrical arcing;
- locally elevated temperatures.
In many of these applications, brazing is a particularly effective technology for joining different materials and producing mechanically strong, repeatable connections.
However, producing a high-quality joint in electrical contact applications requires careful evaluation of the base materials, brazing alloy, joint geometry, heating technique and process control.
This article examines the main requirements of brazing for electrical contact applications and some of the most important aspects to consider when designing the process.
Why Use Brazing in Electrical Contact Applications
Many electrical components are made from different materials selected to perform specific functions.
For example, a component may combine:
- a copper or copper-alloy carrier, selected for its high conductivity;
- a contact material with specific resistance to arcing, wear or high temperatures;
- a filler material used to create the connection between the two elements.
In these cases, brazing makes it possible to create a permanent joint without melting the base materials.
The brazing alloy melts and flows into the joint by capillary action, creating a metallurgical bond between the surfaces.
The main advantages of brazing in electrical contact applications include:
- the ability to join different materials;
- high mechanical strength of the joint;
- good process repeatability;
- lower temperatures than those required to melt the base materials;
- the possibility of automating production;
- compatibility with components of complex geometry;
- precise control of the quantity of brazing alloy used.
Main Requirements of an Electrical Brazed Joint
A joint used in an electrical component normally has to meet several requirements at the same time.
Mechanical Strength
The connection must withstand the stresses generated during component assembly and operation.
Vibration, repeated opening and closing cycles, thermal expansion and mechanical shocks can subject the joint to repeated stresses.
For this reason, the brazing alloy must provide an appropriate combination of:
- strength;
- ductility;
- ability to absorb stresses;
- long-term stability.
Electrical Performance
In electrical contact applications, particular attention must also be paid to the electrical behaviour of the assembly.
The brazed area should not introduce unnecessarily high contact resistance or discontinuities in the current path.
However, it is important to emphasise that joint conductivity depends on the entire system:
- base materials;
- brazing alloy;
- joint geometry;
- thickness of the brazed zone;
- metallurgical quality of the interface.
For this reason, the objective is not simply to select the alloy with the highest possible conductivity, but to design a joint that simultaneously provides suitable electrical, mechanical and manufacturing characteristics.
Resistance to Thermal Cycling
Current flow generates heat.
In addition, many electrical devices operate through repeated on/off cycles.
The brazed joint may therefore be subjected to continuous temperature variations.
When materials with different coefficients of thermal expansion are joined, these variations can generate stresses within the joint.
A sufficiently ductile alloy can help absorb these stresses and reduce the risk of cracking or failure over time.
Materials Used in Electrical Contacts
Electrical contact components use a wide variety of materials.
Common base materials include:
- copper;
- brass;
- copper alloys;
- steels;
- silver-based materials;
- composite materials for electrical contacts.
Contact materials can be selected according to the properties required by the application, such as:
- conductivity;
- arc resistance;
- wear resistance;
- high-temperature stability;
- resistance to contact welding.
The presence of different materials makes it particularly important to evaluate the metallurgical compatibility between the base material, contact material and brazing alloy.
Selecting the Brazing Alloy
Selecting the brazing alloy is one of the most important aspects of process design.
Silver-based brazing alloys are used in many electrical contact applications because they combine:
- excellent wettability;
- good flow characteristics;
- relatively low brazing temperatures;
- high joint reliability;
- good ductility;
- compatibility with many metallic materials.
However, the silver content and alloy composition must be evaluated according to the specific application.
Brazing Temperature
A lower working temperature can be an advantage when components are heat-sensitive.
Reducing heat input can help limit:
- distortion;
- metallurgical changes;
- oxidation;
- damage to other elements in the assembly.
Wettability
The alloy must be able to properly wet the materials to be joined.
Insufficient wetting can result in:
- incomplete filling;
- unbrazed areas;
- reduced strength;
- poorly repeatable results.
Compatibility between the alloy, base material and flux should therefore be evaluated as a complete system.
Ductility
In applications exposed to vibration or thermal cycling, good joint ductility can be a significant advantage.
It helps absorb part of the stresses generated by the different thermal expansion rates of the materials.
Joint Geometry and Capillary Action
As in all brazing applications, joint geometry plays a fundamental role in electrical contact components.
The molten alloy must be able to flow between the surfaces by capillary action.
Incorrect clearance can compromise the process.
Excessive Joint Clearance
This may cause:
- reduced capillary action;
- higher alloy consumption;
- filler metal build-up;
- lower repeatability.
Insufficient Joint Clearance
This may prevent the alloy from fully penetrating the joint.
The design must also consider differences in the thermal expansion of the materials during the brazing cycle.
Heat Control
In the production of electrical components, it is often necessary to limit heating to the areas directly involved in brazing.
Excessive heat input can alter component properties or damage heat-sensitive materials.
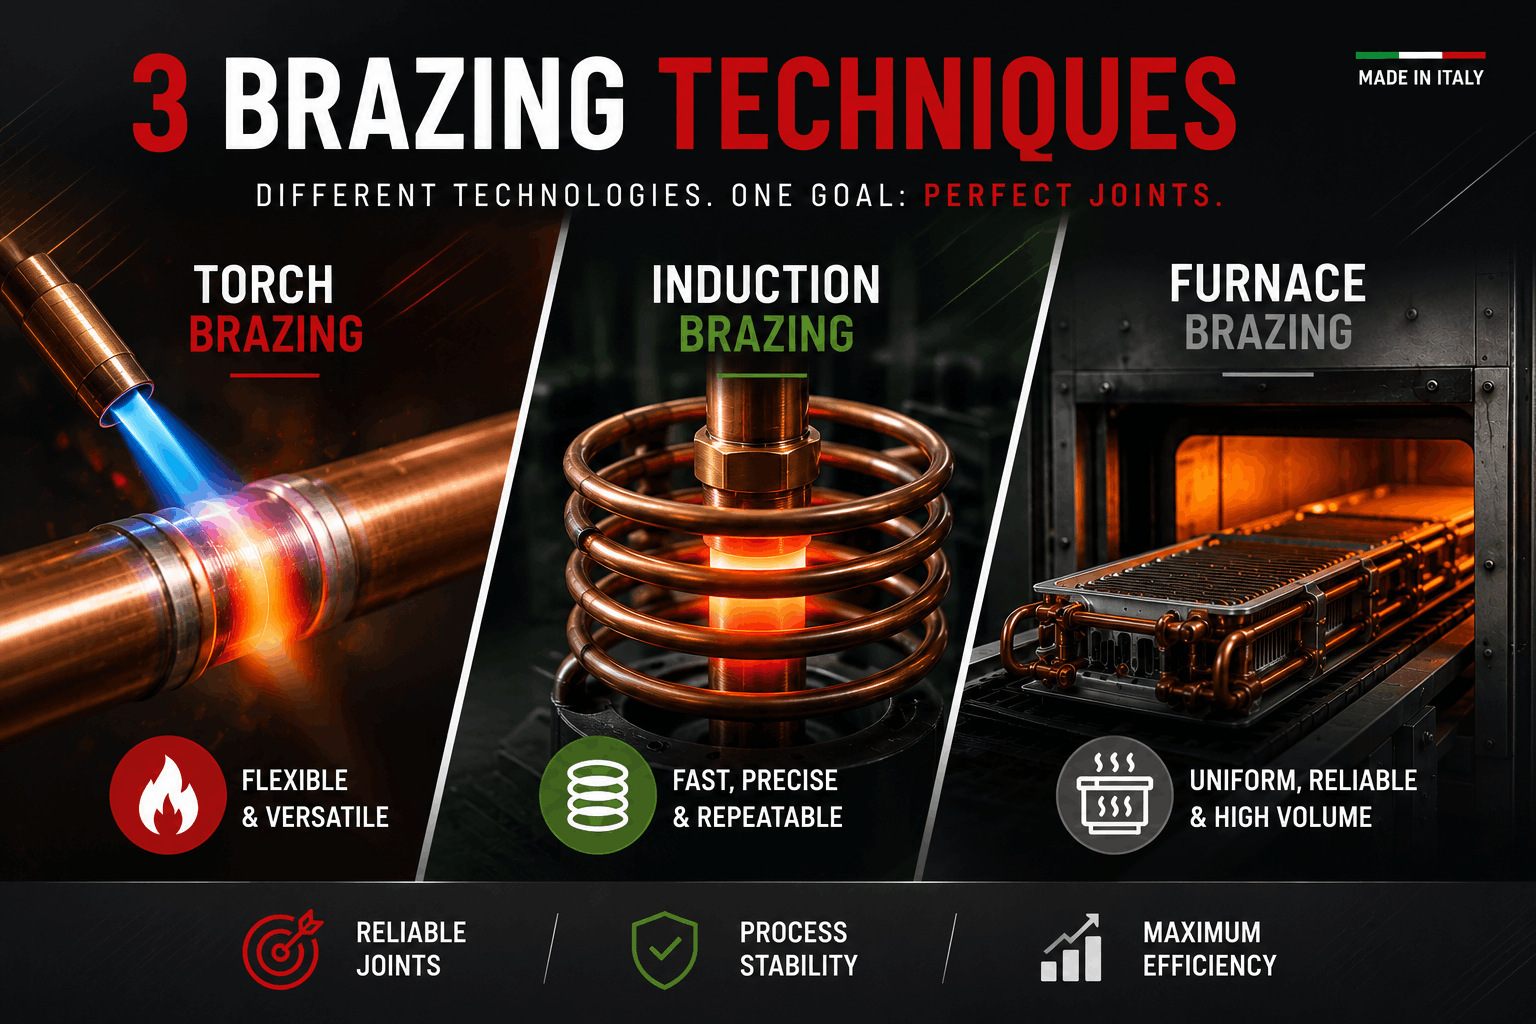
For this reason, different heating techniques are used.
Torch Brazing
Torch brazing can be used for relatively flexible production or larger components.
However, the result depends significantly on operator control.
Induction Brazing
Induction brazing is particularly interesting for electrical contact applications because it provides heating that is:
- rapid;
- localised;
- controllable;
- highly repeatable.
It is also well suited to automation and serial production.
Furnace Brazing
For certain component types and high production volumes, furnace brazing can also be used.
Its main advantage is the high uniformity of the thermal cycle and the possibility of processing many components at the same time.
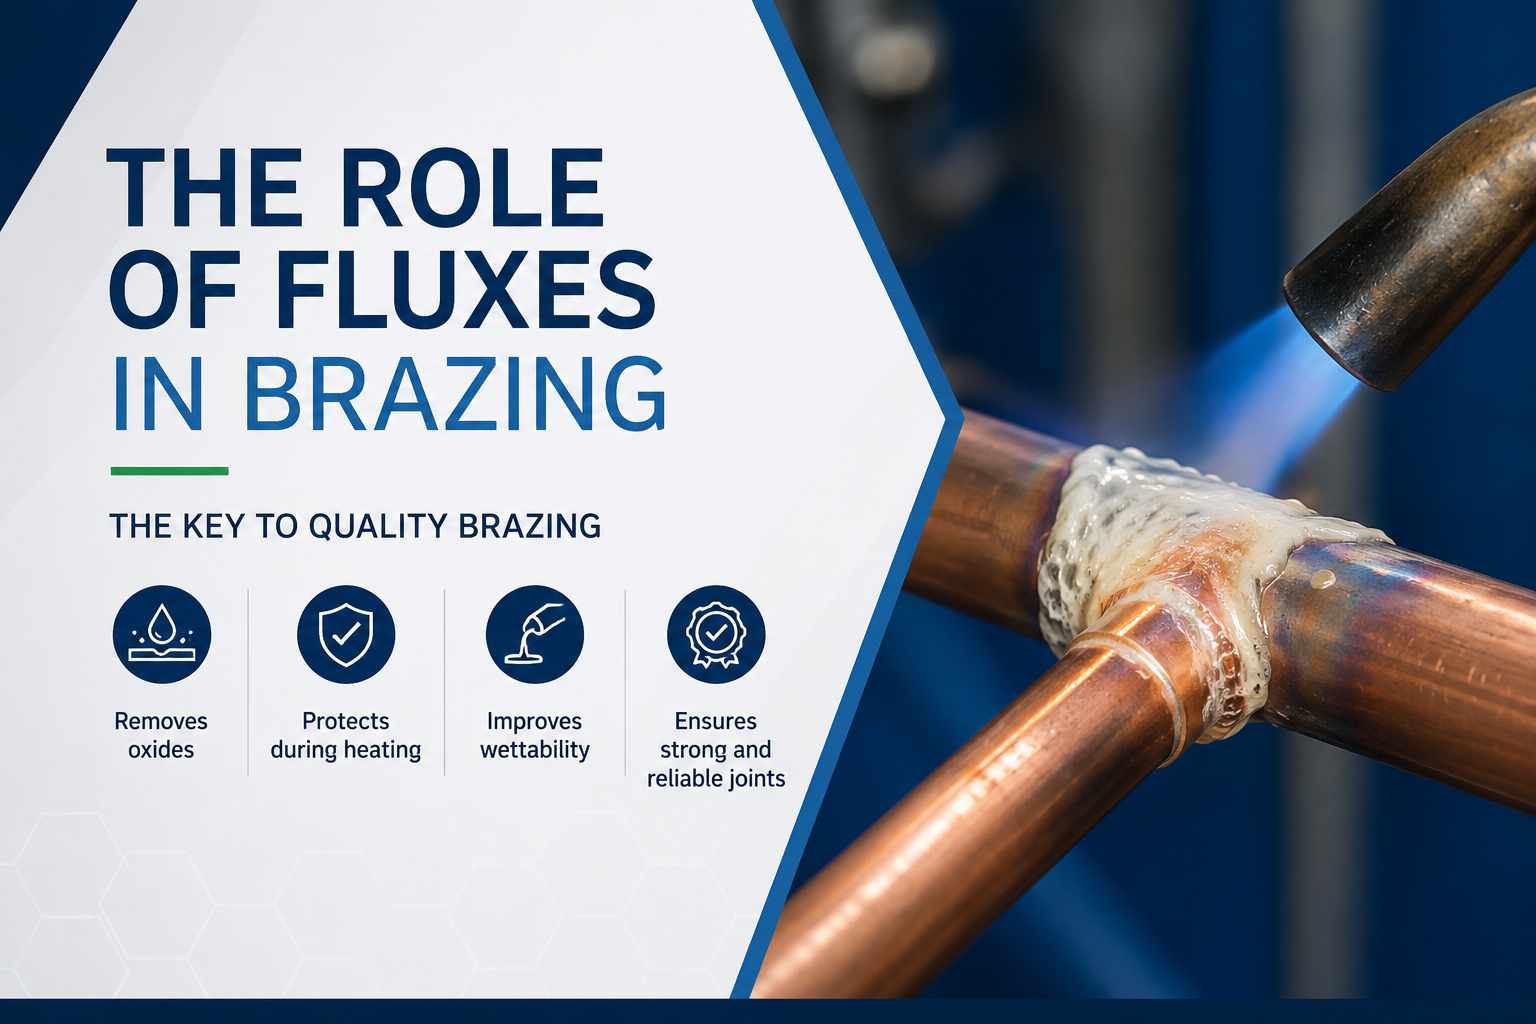
The Role of Fluxes
When brazing is carried out in air, oxide formation can significantly compromise the process.
Brazing flux therefore performs an essential function:
- removing surface oxides;
- protecting materials during heating;
- improving wettability;
- promoting filler metal flow.
Flux selection should consider:
- materials to be joined;
- brazing alloy;
- process temperature;
- heating method;
- any subsequent cleaning requirements.
In processes carried out in controlled atmospheres or under vacuum, the use of flux can be reduced or may not be necessary, depending on the application.
Preforms and Control of Brazing Alloy Quantity
In industrial electrical contact production, one of the most important aspects is repeatability.
Using a variable amount of alloy can create significant differences from one component to another.
For this reason, the following are often used:
- rings;
- washers;
- discs;
- segments;
- custom shapes;
- other types of brazing alloy preforms.
A preform allows a predetermined amount of filler metal to be placed in the joint.
This makes it possible to:
- reduce variability;
- limit excess filler metal;
- improve repeatability;
- simplify automation;
- reduce scrap;
- increase productivity.
The geometry of the preform can also be developed according to the shape of the component to be brazed.
Brazing and Automation
Electrical contact production is often characterised by high volumes.
For this reason, many processes are designed for automation from the outset.
An automated line can control:
| Component positioning | Preform / alloy | Flux | Heating | Time at temperature | Cooling | Final inspection |
Standardising these stages helps reduce differences from one component to another and improves overall process stability.
Typical Applications
Brazing can be used in different components within the electrical and electromechanical sectors.
Typical applications include:
Relays
Joining contact elements and contact materials to their respective metal carriers.
Contactors
Assembly of components designed to handle frequent switching cycles and high currents.
Switches and Protection Devices
Components requiring high mechanical and electrical reliability.
Terminals and Connections
Assemblies in which control of electrical resistance and mechanical robustness is particularly important.
Power Distribution Devices
Components used in switchboards, distribution equipment and industrial systems.
Key Parameters to Control
| Parameter | Possible issue | What to check |
| Surface | Poor wettability | Cleanliness and oxidation |
| Joint clearance | Incomplete filling | Geometry and tolerances |
| Alloy quantity | Build-up or incomplete areas | Dosing / preform |
| Temperature | Alteration of materials | Thermal cycle |
| Flux | Residues or poor wettability | Compatibility and quantity |
| Positioning | Non-uniform joints | Component fixturing |
| Process | Variability | Automation and standardisation |
The same defect can be generated by several causes; for this reason, troubleshooting should always consider the brazing system as a whole.
Joint Quality and Process Control
In electrical components, joint quality should not be evaluated from an aesthetic perspective alone.
Depending on the application, inspections may include:
- correct distribution of the brazing alloy;
- joint filling;
- mechanical strength;
- dimensions and geometry;
- continuity of the connection;
- electrical performance;
- resistance to thermal cycling.
The level and type of inspection should be defined according to the component requirements and service conditions.
Conclusion
Brazing in electrical contact applications requires a balance between mechanical performance, electrical characteristics and production-process stability.
The quality of the result depends on the correct combination of:
- materials to be joined;
- brazing alloy;
- joint geometry;
- flux;
- heating technique;
- alloy quantity;
- thermal-cycle control.
In particular, in high-volume production, the use of preforms and automated processes can significantly improve repeatability and reduce component-to-component variability.
Proper process design therefore makes it possible not only to obtain reliable joints, but also to reduce scrap, improve productivity and increase the reliability of the final device.
Pietro Galliani Solutions for Electrical Contacts
Pietro Galliani offers a range of solutions for electrical and electromechanical applications, with particular attention to the quality and repeatability of industrial processes.
The range includes:
- silver-based brazing alloys;
- alloys available in different melting ranges and compositions;
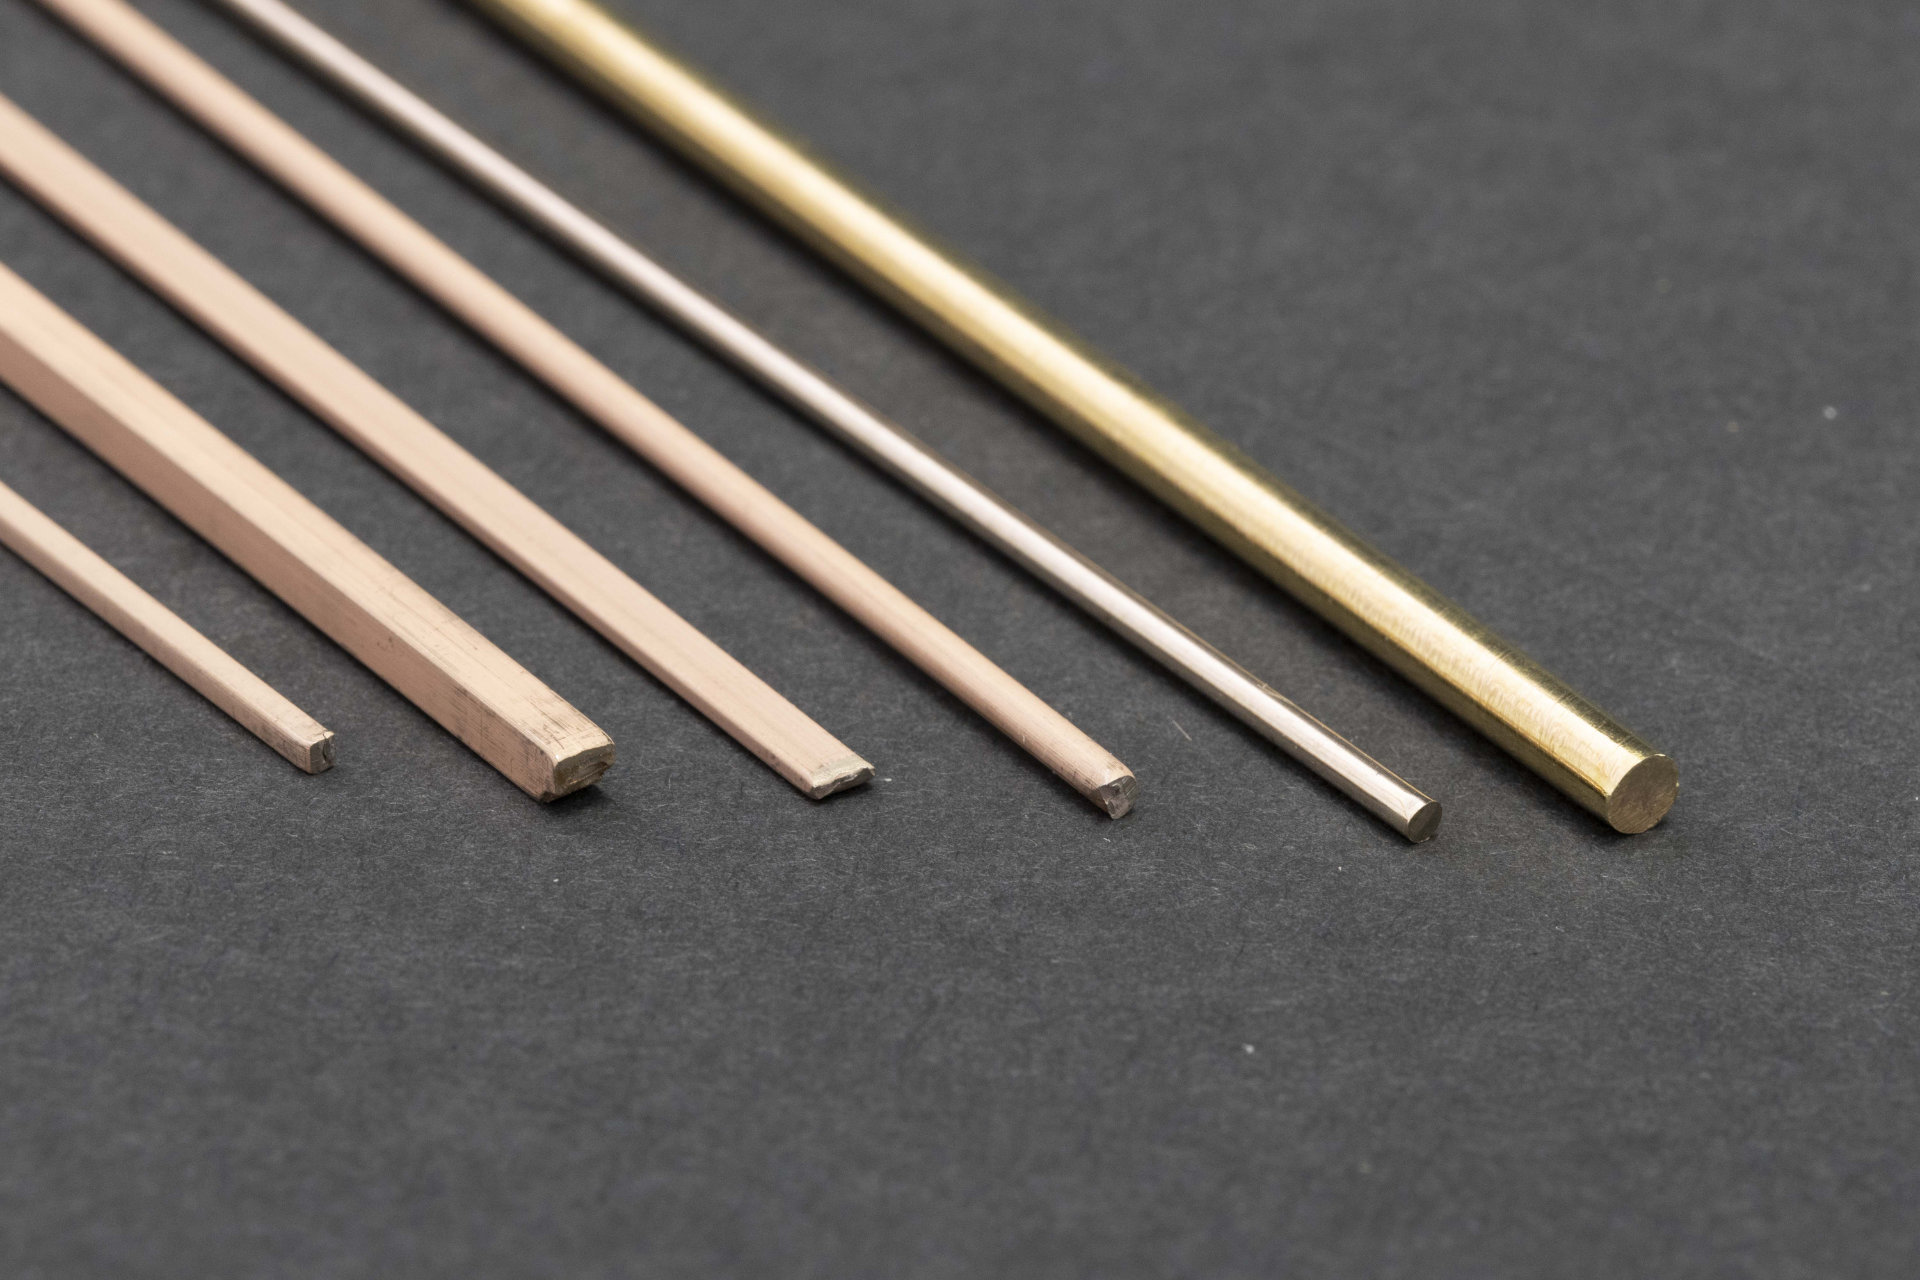
- wires, strips and foils;
- rings and preforms that can be developed according to component geometry;
- GALFLO brazing fluxes;
- solutions for manual and automated processes.
The correct combination of alloy, product form, flux and brazing technology makes it possible to develop more reliable processes tailored to the specific requirements of electrical contact applications.